

A surgical instrument tray is easy to mistake for a simple sheet-metal container. In practice, it has to hold a defined instrument set, protect delicate features, support handling, fit within a chosen storage or transport system, and remain compatible with the customer’s cleaning and processing requirements. Slots, retainers, edges, joints, and drainage features all influence whether the tray is practical to use and manufacture.
Surgical instrument tray fabrication therefore benefits from a design review that connects the instrument layout to the sheet-metal route. The fabrication supplier can help assess bend access, edge condition, joining, surface treatment, and dimensional repeatability. However, the device owner or responsible organization must define the applicable cleaning, sterilization, and validation requirements. This guide explains how to make the geometry easier to quote and build without treating a general tray design as proof of regulatory or process compliance.
Contents
- Start with the instrument set and handling sequence
- Design retainers for location without damage
- Plan sheet-metal geometry around the forming route
- Control edges, joints, and surface requirements
- Coordinate cleaning access and drainage features
- Inspect the tray as an assembled system
- Prepare a clear fabrication package
- Frequently asked questions
Start with the instrument set and handling sequence
Begin with the actual instrument list, not a nominal tray outline. For each instrument, identify the surfaces that may contact the tray, features that must remain protected, the direction in which the instrument is loaded and removed, and whether the user needs visual confirmation of its position. The layout should account for handles, hinges, sharp or delicate ends, cables, and any accessories that travel with the set. Instruments may change across revisions, so the tray drawing should identify the controlled configuration it is intended to hold.
Then map the handling sequence. A tray may be lifted by a rim or handle, stacked with a cover, placed into a case, or moved through a defined processing workflow. Those conditions affect wall height, corner geometry, reinforcement, and access. If the tray nests with another component, define the interface and clearance rather than relying on a rendered model. If labels or identification plates are needed, reserve their location and specify how they are attached without creating an undesirable edge or trapping location.
Use a layout drawing to show instrument position and envelope, while a manufacturing drawing controls the tray itself. Distinguish functional retention dimensions from general clearance. This helps the supplier focus on the few locations that determine fit rather than applying unnecessarily tight tolerances to every sheet-metal dimension.
Design retainers for location without damage
Retainers must restrain the instruments enough for the intended handling condition while allowing deliberate removal. A tight spring tab may hold securely but can obstruct loading, concentrate contact pressure, or fatigue during repeated use. An oversized cutout may make loading easy but allow movement. The right balance depends on instrument geometry, mass, finish, and the expected handling sequence, all of which should be represented in the customer-approved design input.
Review the contact surfaces and edge transitions at each retention point. If a polished, sharp, or delicate instrument feature touches the tray, specify the contact condition and any required protective insert. If polymer retainers or pads are used, their material, attachment, replacement, and compatibility requirements should be defined separately; the fabricator should not choose a polymer based solely on appearance. For prototypes, a physical fit check with representative instruments can reveal whether tabs are reachable and whether the parts sit in the intended orientation.
Try to avoid retainers that depend on an unmeasured deflection or an undocumented force. If retention force is a controlled requirement, the test method and acceptance range should be provided by the design owner. For simpler designs, an agreed functional fit inspection may be more appropriate. The important point is to distinguish a purposeful retention feature from a purely decorative cutout.
Plan sheet-metal geometry around the forming route
Flat patterns, bend lines, hems, tabs, corners, and cutouts should be considered together. A hole too close to a bend may distort, a narrow flange may be difficult to form consistently, and a corner relief that is too small can create tearing or an unwanted sharp edge. The material thickness, alloy and condition, grain direction where relevant, inside radius, tooling, and quantity all influence the practical design window. These details should be resolved against the specified material and the supplier’s process rather than assumed from a generic rule.
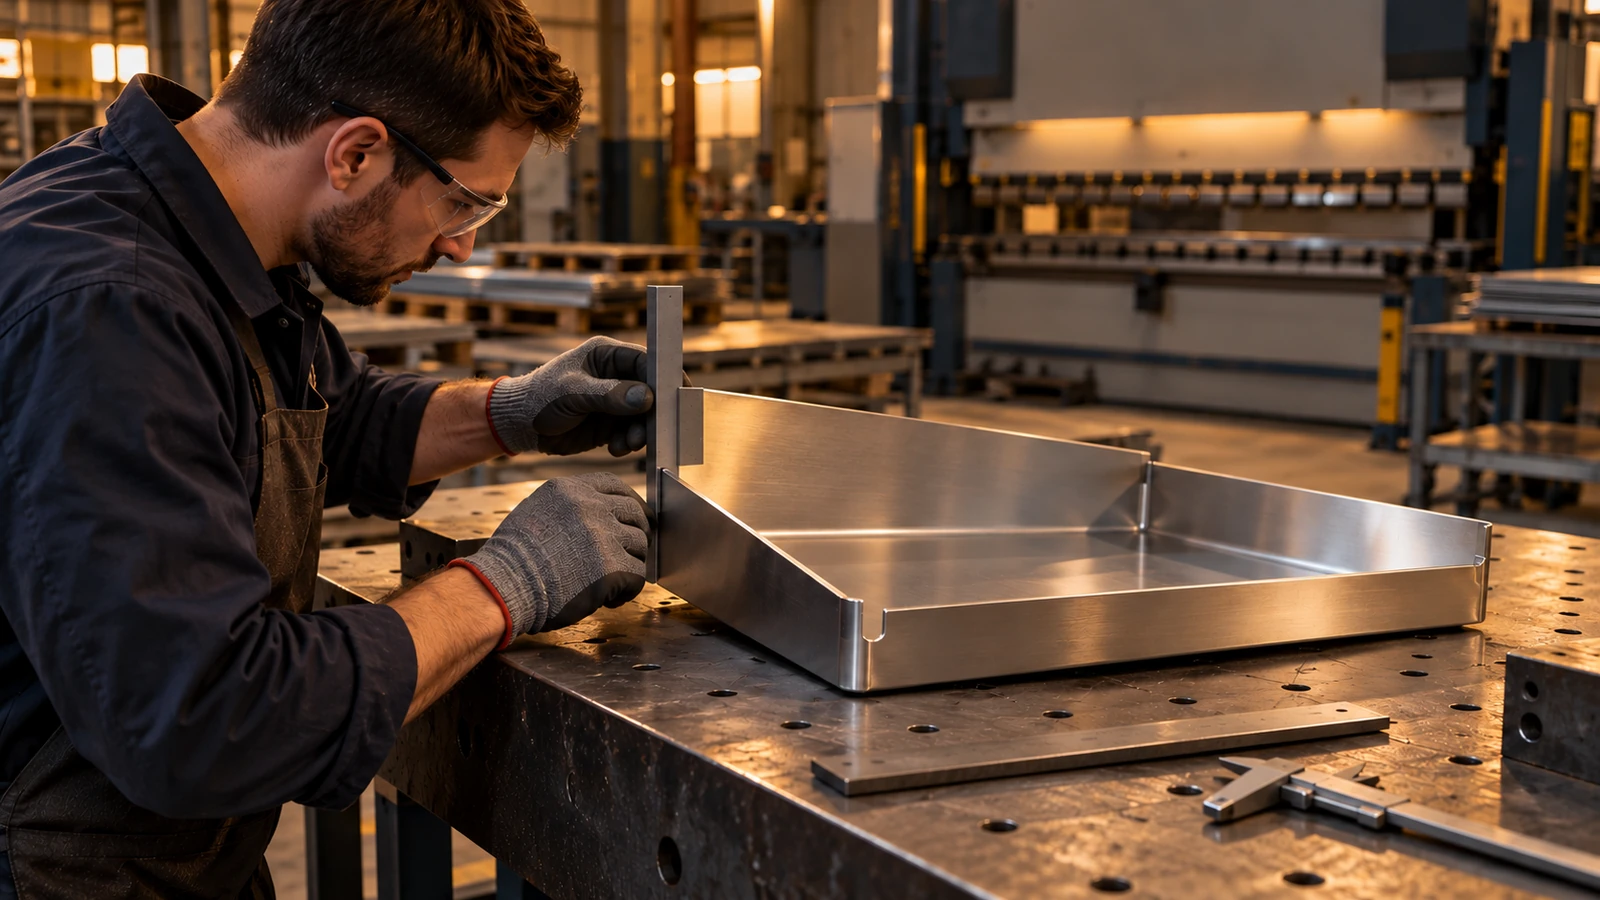
For a formed tray, identify critical wall angles, overall envelope, flatness or seating requirements, and interfaces to covers or cases. Add relief where it supports the chosen bend sequence, but keep the resulting edge and corner condition consistent with use. If the design uses multiple formed pieces, consider how their datums meet during assembly. Welds, fasteners, or other joining methods may introduce heat, distortion, access constraints, or surfaces that need post-process finishing.
| Caractéristique | Manufacturing question | Drawing information to clarify |
|---|---|---|
| Bend and flange | Can the geometry be formed with available tool access? | Material, thickness, radius, angle, and critical envelope |
| Slot near a bend | Will forming distort the opening or weaken the flange? | Slot location, size, edge condition, and functional clearance |
| Corner and relief | Can the corner be formed and finished without an unsafe edge? | Relief geometry and acceptable edge condition |
| Joined feature | Can the joint be accessed, inspected, and cleaned as intended? | Joint location, appearance or strength criteria, and inspection scope |
When the geometry is still under development, a prototype can test instrument fit, loading sequence, stack interfaces, and handling before the flat pattern is released. The site’s prototyping service is relevant when a team needs physical samples for design learning. For the production route, compare the design with the site’s sheet metal fabrication capabilities and identify any features that need adjustment.
Control edges, joints, and surface requirements
Edge condition is a functional and handling concern. Laser-cut or punched profiles may need deburring, edge rounding, or a specified finish, especially where hands, instruments, or protective packaging contact them. State whether sharp edges, loose burrs, dross, or visible tool marks are acceptable and identify the regions where the requirement is critical. A blanket note may be appropriate for safety, but it should not replace a tighter requirement at a contact or mating surface.
Joining decisions should account for both structural needs and cleaning access. A continuous seam can close a gap but may also create heat distortion or a surface that needs additional finishing. A mechanical joint may be serviceable but can introduce fasteners and interfaces that must be controlled. Select the method from the design and use requirements; do not assume that a particular weld or fastener is universally preferred.
Material and surface treatment must be specified for the intended environment. Stainless steel is often considered for particular corrosion and cleaning conditions, but grade, condition, finish, and compatibility still need approval. Other materials may be suitable where the design and process requirements allow them. The site’s stainless steel material information et surface finishing service overview can inform an early conversation. They do not establish that a given tray is validated for a specific cleaning agent or sterilization cycle.
Coordinate cleaning access and drainage features
Cleaning and processing requirements must come from the device owner, hospital, or other responsible organization. The fabrication drawing can support those requirements by avoiding inaccessible pockets, defining drain or vent openings where needed, and specifying surface and edge conditions. But a design feature that appears easy to rinse is not proof that a cleaning process is effective. Process validation and acceptance criteria are separate from ordinary dimensional fabrication.
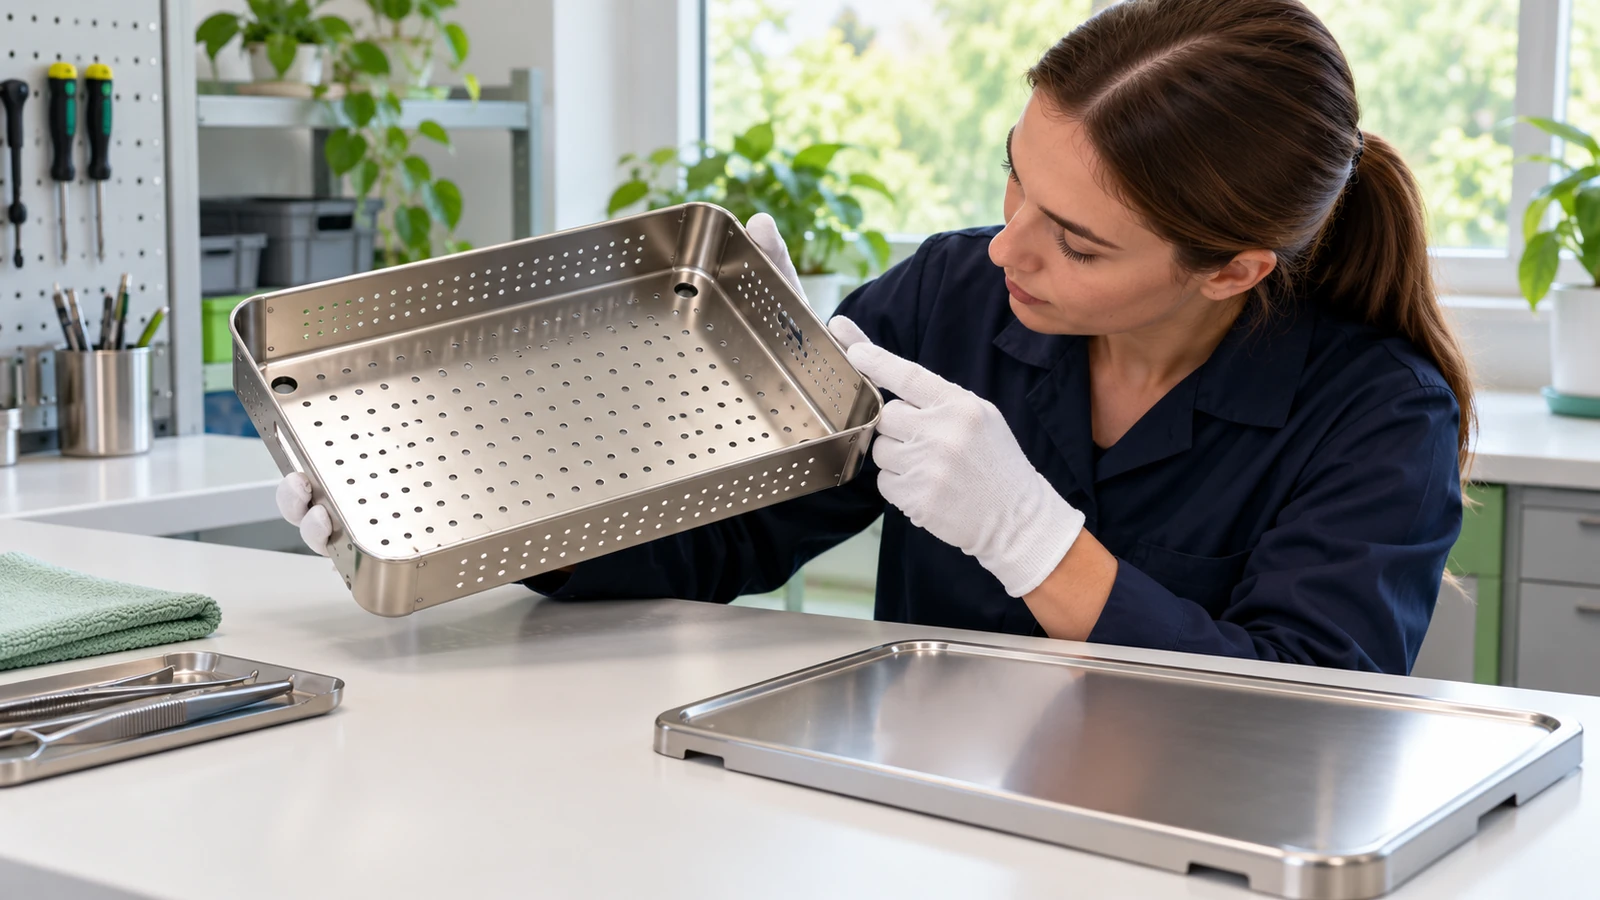
Review whether liquid or debris could collect at hems, enclosed corners, joints, retainers, or under an instrument. If the tray is intended to drain, identify the required orientation and the locations that must remain open. If it is used with a cover or mat, review the complete assembly because the adjacent part may block an opening. The geometry should be assessed in the intended configuration rather than as a bare tray alone.
Packaging and identification also matter. The finished surface can be damaged or contaminated during handling if parts contact each other or if labels shed residue. Specify the protection method, labeling content, lot or revision identification, and any cleanliness evidence required at delivery. If the customer has a controlled cleaning or sterilization validation protocol, reference the approved document and revision rather than summarizing it loosely in a supplier note.
Inspect the tray as an assembled system
Inspection can cover overall dimensions, formed angles, flatness or seating, opening locations, joint condition, edge requirements, and fit with representative instruments or mating hardware. Decide which dimensions need recorded results and which can be verified through a functional fixture. The datum setup should reflect how the tray is used or assembled; measuring a flexible tray while it is unsupported can produce results that are not representative of its functional condition.
A fit check should use identified instrument models or controlled envelopes. Record whether the tray accepts each item, whether retainers engage, whether items can be removed without interference, and whether the assembly fits its cover or case. If a force, drop, vibration, or transport test is required, the customer should define the fixture, conditioning, sample plan, and acceptance criteria. Do not imply that a simple shop fit check demonstrates all handling or sterilization performance.
For multiple-piece trays, inspect the assembled configuration as well as individual components. Joining may alter flatness or alignment, and hardware may protrude into an instrument space. If cosmetic criteria matter, define the viewing condition and acceptable locations rather than relying on subjective language. Link results to part revision and lot identity so a later change can be traced.
Prepare a clear fabrication package
A useful RFQ includes the instrument list or controlled envelopes, a dimensioned tray drawing, revision, material and thickness, finish notes, quantity, tolerance requirements, assembly interfaces, and packaging expectations. Add a flat-pattern view or model when available, and identify whether the model is reference geometry or the released authority. Call out critical bends, slots, retainers, contact points, and drain features. Include the required inspection report level and any customer-controlled processing documents.
Ask the supplier to review the bend sequence, tool access, relief geometry, joining route, edge finishing, and inspection setup. Request that assumptions and exclusions be stated in the quote. If the supplier suggests changing a tab, corner, or slot, evaluate how the proposal affects instrument fit and handling before accepting it. A manufacturing simplification is useful only if it preserves the intended function.
During design changes, revise the drawing and instrument configuration together. A tray updated for one new instrument may leave another item unsupported. Define revision identification on the part or delivery documentation so receiving teams can distinguish versions. This prevents a visually similar tray from being used with an unintended set.
Frequently asked questions
Does a fabricated tray automatically meet sterilization requirements?
No. Fabrication can meet defined material, geometry, finish, and documentation requirements. Compatibility and validation for a particular cleaning or sterilization process must be defined and verified by the responsible organization.
Which material should be used for a surgical instrument tray?
The device specification and intended environment determine the material. Consider corrosion, cleaning, stiffness, weight, joining, finish, and contact with instruments; confirm the exact grade and condition before production.
Should retainers be included in the sheet-metal design?
They can be integral formed features or separate components, depending on function, replacement needs, material compatibility, and manufacturing route. The design should define their contact, retention behavior, and inspection criteria.