


L'aluminium est le matériau le plus polyvalent dans le monde de la fabrication. À l'état brut, il est léger, conducteur et facile à usiner, mais il reste sensible aux effets ternissants de l'oxydation atmosphérique et de l'usure de surface. Pour transformer ce métal tendre en un composant industriel haute performance, les ingénieurs comptent sur l' aluminium anodisé. Il ne s'agit pas simplement d'un revêtement ; c'est une transformation électrochimique qui convertit la surface du métal en un bouclier durable en oxyde d'aluminium semblable à de la céramique. Ce procédé est la pierre angulaire de la fabrication moderne traitement de surface par usinage CNC, offrant un mélange unique d'esthétique vibrante et de protection mécanique.

Chez Jucheng Precision, nous comprenons qu'une finition anodisée réussie se décide dans la fraiseuse CNC, pas seulement dans le bain chimique. Nous traitons l'anodisation comme un défi géométrique où l'épaisseur, le masquage et la pureté du matériau dictent l'ajustement final de l'assemblage. Que vous développiez un boîtier élégant pour l'électronique grand public ou un piston hydraulique à forte usure, maîtriser les nuances de la couche anodique est essentiel. Ce guide explore la différence technique entre les finitions décoratives et les revêtements durs, l'importance cruciale du masquage stratégique, et comment JUCHENG intègre ces processus pour livrer des composants "prêts à installer" à nos partenaires mondiaux dans les secteurs aérospatial, médical et automobile.
La cohérence dans la finition nécessite une maîtrise à la fois de la physique et de la chimie. Vous ne pouvez pas simplement tremper une pièce et vous attendre à ce qu'elle brille ; vous devez concevoir la surface dès la première trajectoire d'outil. Examinons les piliers techniques qui font de l'anodisation le choix privilégié pour la protection de l'aluminium.
contenu :
Excellence décorative : L'art de l'anodisation de type II
Armure dure : Survivre grâce à l'ingénierie avec le type III
Masquage stratégique : Protection des filetages et des points de mise à la terre
Logique dimensionnelle : Gestion de la croissance et des tolérances
Stratégie chromatique : Contrôle de la couleur entre les lots
Hub intégré de JUCHENG : De la billette au bain
Excellence décorative : L'art de l'anodisation de type II

L'anodisation de type II est la variante la plus populaire de l' aluminium anodisé, principalement axée sur la résistance à la corrosion et l'attrait esthétique. Dans ce procédé, la pièce en aluminium est immergée dans un bain d'acide sulfurique et soumise à un courant électrique précis. Cela crée une fine couche transparente d'oxyde d'aluminium, généralement entre 5 et 25 microns d'épaisseur. La caractéristique du type II est sa structure microscopique ; la couche d'oxyde se développe selon un motif hexagonal en nid d'abeille, laissant des millions de petits pores ouverts. Ces pores sont la clé de la polyvalence visuelle du matériau.
During the dyeing stage, specialized organic or inorganic pigments are drawn into these open pores. Because the color is "inside" the material rather than on the surface, it is significantly more durable than paint or powder coating. It cannot chip or peel. After dyeing, the parts are "sealed" in boiling water or a chemical bath, which causes the hexagonal cells to swell and close, locking the color and the corrosion resistance in place permanently. Jucheng Precision offers a vast array of Type II colors—from deep tactical blacks to brilliant blues and reds—ensuring that your consumer-facing products carry a premium, jewel-like finish that reflects the quality of the internal engineering. This process is ideal for handheld devices, camera housings, and medical enclosures where both hygiene and beauty are mandatory.
Armure dure : Survivre grâce à l'ingénierie avec le type III

When aesthetics take a backseat to raw physical survival, we turn to Type III, more commonly known as "Hardcoat Anodizing." While the basic chemistry is similar to Type II, the execution is far more extreme. The electrolyte bath is chilled to near-freezing temperatures (0°C to 10°C), and the electric current is significantly increased. This "cold-bath" process forces the oxide layer to grow much more densely and to a much greater thickness—typically ranging from 25 to 100 microns. The result is a surface that rivals the hardness of case-hardened steel or industrial ceramics.
A Type III aluminium anodisé surface provides exceptional wear resistance, making it suitable for dynamic components like pulleys, gear teeth, and sliding valve bodies. It is also an incredibly effective electrical insulator, often used to prevent grounding in high-voltage assemblies. Because the layer is so dense, it is naturally dark—usually appearing as a charcoal grey, bronze, or deep olive green. While it can be dyed black, the natural dark hue of hardcoat prevents light, vibrant colors. At Jucheng Precision, we recommend Type III for your most brutal mechanical applications. We manage the high heat-load of the hardcoat process to ensure that even thin-walled aluminum parts do not warp during the intense electrochemical reaction, providing an "armored" finish that stands the test of industrial time.
Masquage stratégique : Protection des filetages et des points de mise à la terre
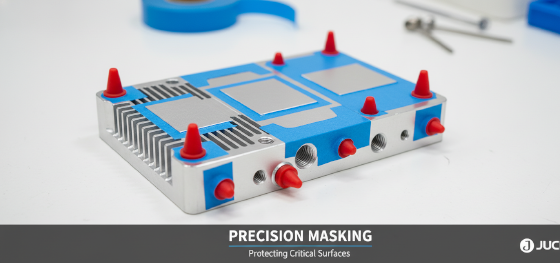
The greatest challenge in anodizing is its non-selective nature. The acid bath and the electric current will attack every exposed square millimeter of the aluminum. However, an aluminum oxide layer is a powerful electrical insulator. If your part requires an EMI shielding contact or a grounding point, an anodized surface will prevent the assembly from working. Furthermore, the buildup of the oxide layer can ruin tight-tolerance internal threads, making it impossible to install fasteners. Precision manufacturing requires the ability to choose exactly where the anodizing stops.
Jucheng Precision solves this through a rigorous, engineered masking protocol. We utilize high-temperature liquid masks, specialized silicone plugs, and custom-cut Kapton tapes to shield critical features. We identify "Conductive Zones" and "Precision Bores" during our DFM review. Our technicians are experts at applying these masks with surgical precision, ensuring that after the bath, the protected areas remain raw, conductive aluminum. We also pay close attention to "Acid Traps"—hidden pockets or blind holes where acid can remain trapped after the rinse cycles. If not managed, this trapped acid will "bleed out" later, destroying the finish of the part. By engineering the masking and the rinsing cycle together, we deliver complex, multi-functional parts that are ready for immediate assembly in the most sensitive electronic systems.
Logique dimensionnelle : Gestion de la croissance et des tolérances

One of the most frequent misconceptions in aluminium anodisé is that it is a "coating" that sits on top of the metal. In reality, it is a conversion. For every unit of thickness the oxide layer adds, roughly 50% of that thickness is grown "outward" and 50% is consumed "inward" into the base metal. This is the "50/50 Rule" of anodizing growth. If you specify a 20-micron Type II finish, your part will physically grow by 10 microns per surface, increasing a diameter by 20 microns. For a Type III finish of 50 microns, the part grows by 25 microns per side.
At Jucheng Precision, we eliminate the guesswork by providing DFM advice on "Pre-Finish Machining." For parts with +/- 0.01mm tolerances, we machine the raw aluminum slightly undersized to account for the calculated growth of the anodic layer. This ensures that when the part comes out of the bath, it "grows" into the center of your tolerance zone. We utilize digital eddy-current thickness gauges to verify the layer depth on every batch, ensuring that the dimensions on your print are met perfectly in the finished state. This integration of machining and finishing logic is what separates JUCHENG from standard shops that simply "cut and dip," reducing your risk of assembly failure and costly rework.
Stratégie chromatique : Contrôle de la couleur entre les lots

In a global supply chain, "Blue" is not a technical specification. Achieving color consistency in aluminium anodisé is notoriously difficult because the final hue is influenced by multiple variables: the specific alloy (6061 vs 7075), the bath temperature, the dye concentration, and the immersion time. If a set of mating parts is anodized in two different batches, they might arrive with slightly different shades, ruining the visual cohesion of your product. For brands like Apple or high-end automotive suppliers, this inconsistency is a major quality failure.
Jucheng Precision manages this through a "Chromatic Strategy." We utilize digital spectrophotometers to measure the LAB color values of our finishes, ensuring they fall within a strict Delta-E tolerance range. We maintain dedicated "Color Standards" for our long-term clients, allowing us to match batches produced years apart. We also emphasize the importance of "Lot Segregation"—ensuring that all parts for a single assembly are processed in the same bath at the same time to guarantee a 100% visual match. Our expertise in the chemistry of the bath ensures that the "Electric Blue" or "Gunmetal Grey" you approved in the prototype phase is the exact same color you receive in mass production. We bridge the gap between industrial utility and luxury aesthetics.
Hub intégré de JUCHENG : De la billette au bain

The biggest risk in high-end aluminum manufacturing is the fragmentation of the supply chain. If you buy machining from one vendor and anodizing from another, who is responsible if the part warps or the color is wrong? Jucheng Precision eliminates this risk by serving as an integrated hub for aluminum excellence. Our facility is designed to move parts seamlessly from our high-speed 5-axis CNC centers directly into our finishing lines. We manage the entire lifecycle: from the initial alloy verification via spectrometer to the final CMM inspection of the anodized surfaces.
Our integrated approach ensures that the surface finish is treated with the same technical rigor as the tool paths. We understand that for an aerospace connector or a medical instrument, the "Anodic Seal" is a critical safety parameter. We perform "Seal Integrity" tests to ensure the part is fully passive and ready for harsh environments. When you receive a component from JUCHENG, it is a fully verified engineering solution—machined to perfection and armored for survival. For more details on the materials we use, visit our CNC Aluminum Machining hub. Whether you need the decorative brilliance of Type II or the industrial armor of Type III, Jucheng Precision has the expertise to bring your designs into the light. Contact our engineering team today for a comprehensive technical review of your next aluminium anodisé project.

